
Chapter 12
Hydraulic & Pneumatic Power Systems
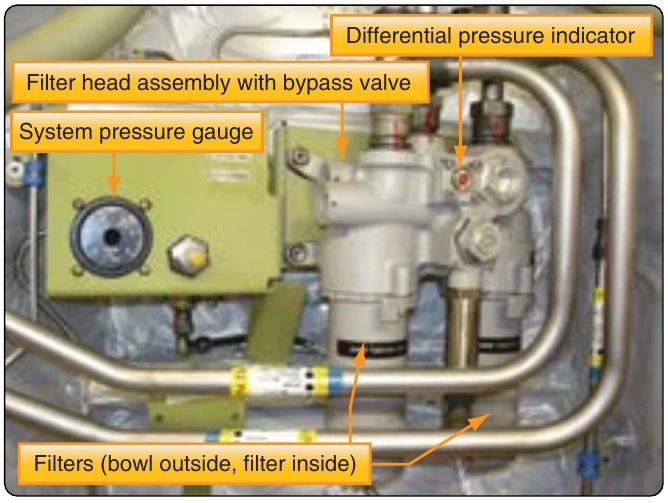
The element may be a micron, porous metal, or magnetic type. The micron element is made of a specially treated paper and is normally thrown away when removed. The porous metal and magnetic filter elements are designed to be cleaned by various methods and replaced in the system.
Micron-Type Filters
A typical micron-type filter assembly utilizes an element made of specially treated paper that is formed in vertical convolutions (wrinkles). An internal spring holds the elements in shape. The micron element is designed to prevent the passage of solids greater than 10 microns (0.000394 inch) in size. [Figure 12-17] In the event that the filter element becomes clogged, the spring-loaded relief valve in the filter head bypasses the fluid after a differential pressure of 50 psi has been built up. Hydraulic fluid enters the filter through the inlet port in the filter body and flows around the element inside the bowl. Filtering takes place as the fluid passes through the element into the hollow core, leaving the foreign material on the outside of the element.
Maintenance of Filters
Maintenance of filters is relatively easy. It mainly involves cleaning the filter and element or cleaning the filter and replacing the element. Filters using the micron-type element should have the element replaced periodically according to applicable instructions. Since reservoir filters are of the micron type, they must also be periodically changed or cleaned. For filters using other than the micron-type element, cleaning the filter and element is usually all that is necessary. However, the element should be inspected very closely to ensure that it is completely undamaged. The methods and materials used in cleaning all filters are too numerous to be included in this text. Consult the manufacturer’s instructions for this information.
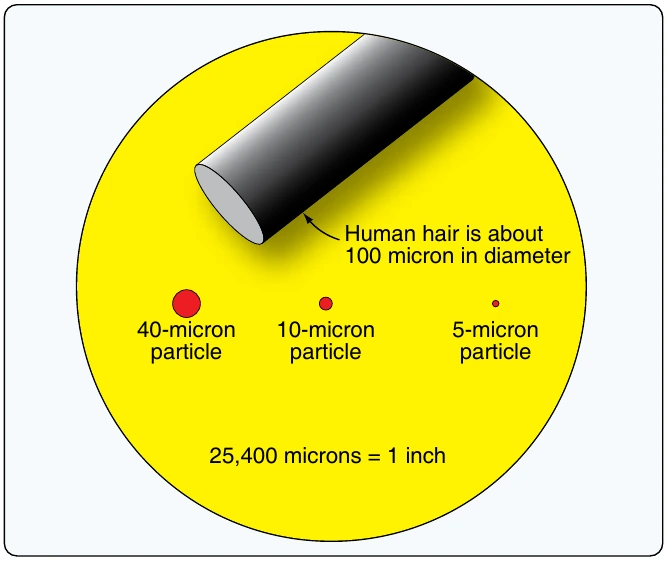
When replacing filter elements, be sure that there is no pressure on the filter bowl. Protective clothing and a face shield must be used to prevent fluid from contacting the eye. Replace the element with one that has the proper rating. After the filter element has been replaced, the system must be pressure tested to ensure that the sealing element in the filter assembly is intact.
In the event of a major component failure, such as a pump, consideration must be given to replacing the system filter elements, as well as the failed component.
Filter Bypass Valve
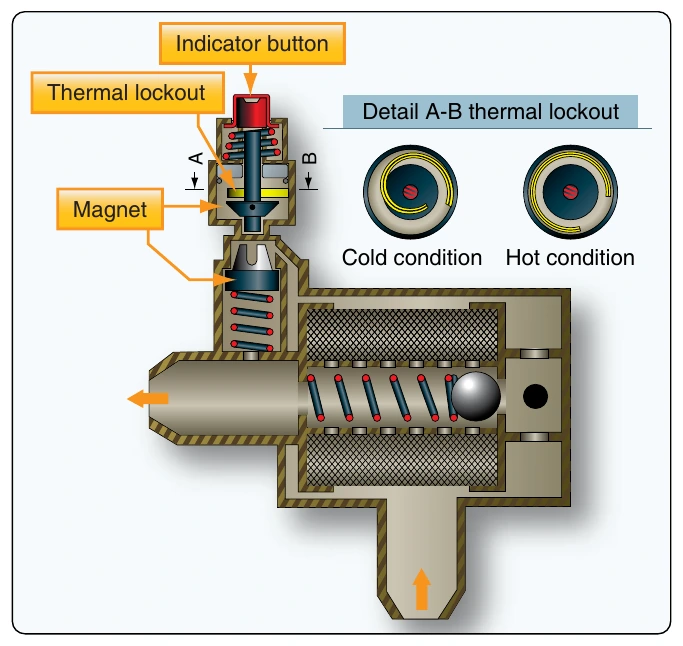
Filter modules are often equipped with a bypass relief valve. The bypass relief valve opens if the filter clogs, permitting continued hydraulic flow and operation of aircraft systems. Dirty oil is preferred over no flow at all. Figure 12-18 shows the principle of operation of a filter bypass valve. The ball valve opens when the filter becomes clogged and the pressure over the filter increases.
Filter Differential Pressure Indicators
The extent to which a filter element is loaded can be determined by measuring the drop in hydraulic pressure across the element under rated flow conditions. This drop, or differential pressure, provides a convenient means of monitoring the condition of installed filter elements and is the operating principle used in the differential pressure or loaded-filter indicators found on many filter assemblies.
Differential pressure indicating devices have many configurations, including electrical switches, continuous-reading visual indicators (gauges), and visual indicators with memory. Visual indicators with memory usually take the form of magnetic or mechanically latched buttons or pins that extend when the differential pressure exceeds that allowed for a serviceable element. [Figure 12-18, top] When this increased pressure reaches a specific value, inlet pressure forces the spring-loaded magnetic piston downward, breaking the magnetic attachment between the indicator button and the magnetic piston. This allows the red indicator to pop out, signifying that the element must be cleaned. The button or pin, once extended, remains in that position until manually reset and provides a permanent (until reset) warning of a loaded element. This feature is particularly useful where it is impossible for an operator to continuously monitor the visual indicator, such as in a remote location on the aircraft.
Some button indicators have a thermal lockout device incorporated in their design that prevents operation of the indicator below a certain temperature. The lockout prevents the higher differential pressure generated at cold temperatures by high fluid viscosity from causing a false indication of a loaded filter element.
Differential pressure indicators are a component part of the filter assembly in which they are installed and are normally tested and overhauled as part of the complete assembly. With some model filter assemblies, however, it is possible to replace the indicator itself without removal of the filter assembly if it is suspected of being inoperative or out of calibration. It is important that the external surfaces of button-type indicators be kept free of dirt or paint to ensure free movement of the button. Indications of excessive differential pressure, regardless of the type of indicator employed, should never be disregarded. All such indications must be verified and action taken, as required, to replace the loaded filter element. Failure to replace a loaded element can result in system starvation, filter element collapse, or the loss of filtration where bypass assemblies are used. Verification of loaded filter indications is particularly important with button-type indicators as they may have been falsely triggered by mechanical shock, vibration, or cold start of the system. Verification is usually obtained by manually resetting the indicator and operating the system to create a maximum flow demand ensuring that the fluid is at near normal operating temperatures.
Pumps
All aircraft hydraulic systems have one or more power-driven pumps and may have a hand pump as an additional unit when the engine-driven pump is inoperative. Power-driven pumps are the primary source of energy and may be either engine driven, electric motor driven, or air driven. As a general rule, electrical motor pumps are installed for use in emergencies or during ground operations. Some aircraft can deploy a ram air turbine (RAT) to generate hydraulic power.